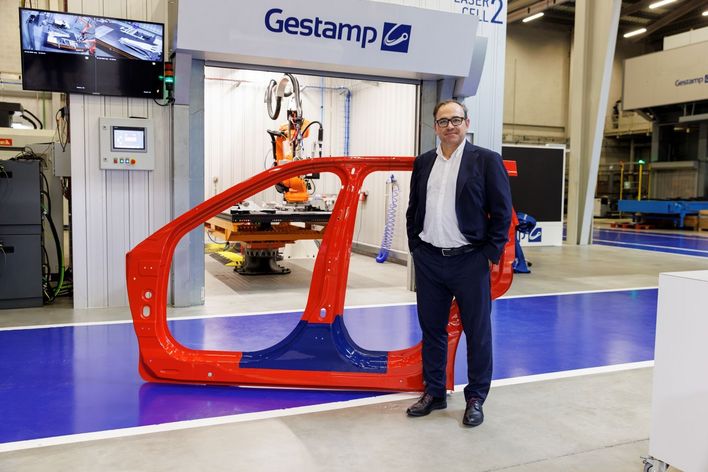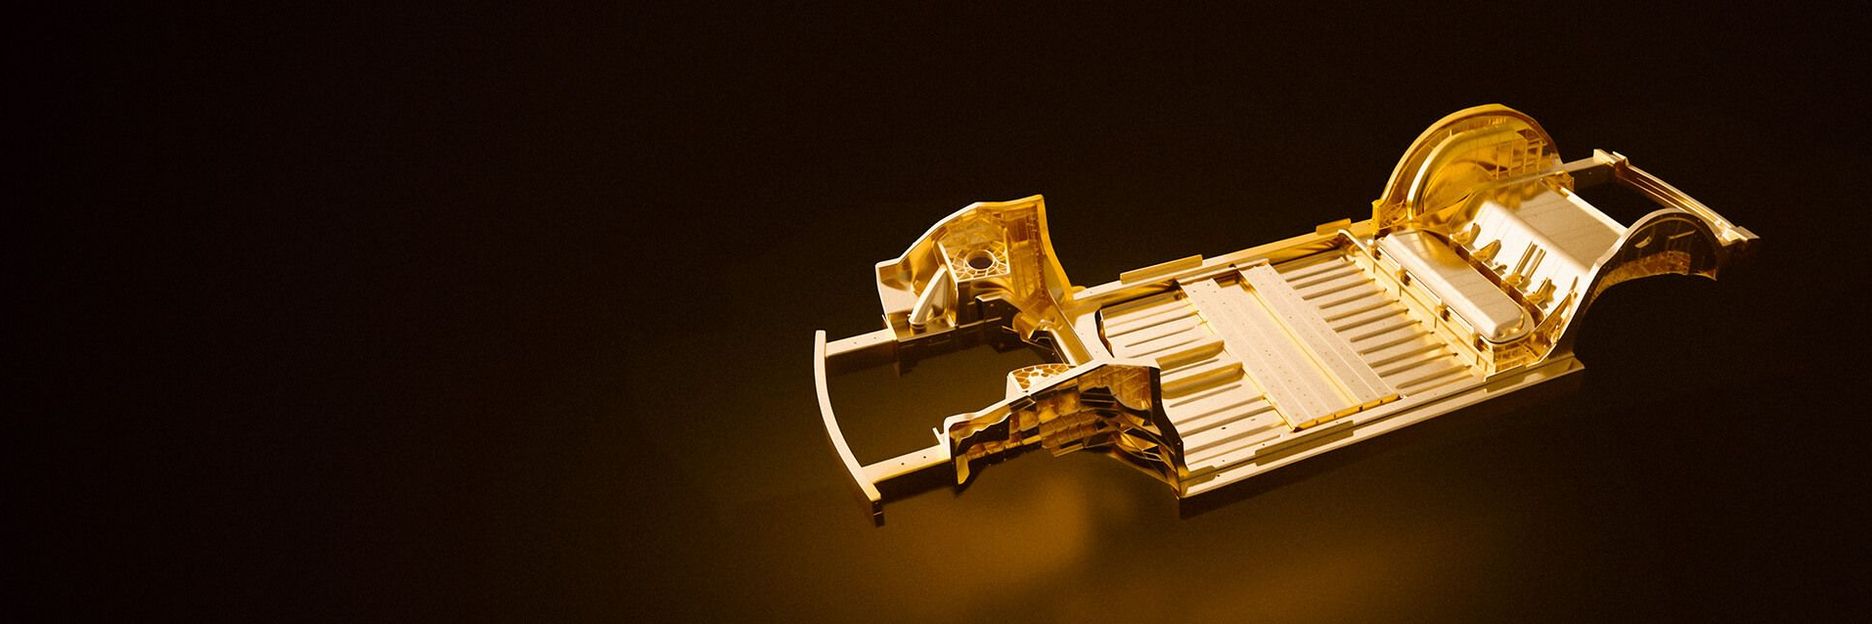
Gigacasting: a manufacturing technology whereby a single solid aluminum casting process replaces a hundred or more single parts. This does not just save time – assembly takes just 90 to 120 seconds instead of 45 minutes – but also reduces costs, material, and weight. The automotive industry makes extensive use of this technology to manufacture vehicle assemblies more easily and cost-effectively, especially in electric vehicles, where every kilogram counts. However, post-processing is complex: excess material and burrs must be removed, and surfaces must be cleaned and all of this must be completed reliably and quickly in large volumes. This is where the laser comes into play with four specialized solutions.
Overview of four post-processing solutions
Degating – removing excess material:
When the die-cast part comes out of the mold and quenching tank, there are still 10 to 30 odd-looking structures protruding from its outer contours: thin legs with feet attached or flat discs, usually, simply referred to as "gates" in technical jargon. These are made up of solidified aluminum in the feed channels leading to the casting mold and are two to six millimeters thick. The first post-processing step is to remove these rough remnants.
Laser solution: Light from high-power lasers with six or more kilowattscuts the excess material off. Thanks to the high kilowatt power, the cut is extremely precise and is also completed so quickly that only a minimal amount of heat penetrates the aluminum component, preventing it from deforming. On the production line, this task is either performed by six-axis robots equipped with optics for remote cutting or a cutting head in a laser cell with a rotary table.
Deburring & hole-making:
Regardless of how high the clamping force of the casting machine may be, the molten aluminum still seeps into the tiniest gaps where the two halves of the mold meet. Paper-thin, sharp burrs are generated, which can reach a total length of eight meters. In addition, the components require dozens of holes and recesses for subsequent assembly.
Laser solution: Lasers located in the processing cell or guided by a robot via a scanner move along the contours removing all excess material. For this type of precision work, a very bright beam is more important for achieving an optimum ratio of processing speed and quality than sheer laser power. Laser beams with a brightness of two BPP (Beam Parameter Product) remove burrs and cut mounting holes with millimeter precision.
Marking (traceability, data matrix code):
Since gigacasting often replaces hundreds of small components with a single large one, achieving top-notch traceability is actually quite easy. A single data matrix code is all it takes for smart factories to link an individual component to a database containing all the key parameters of the casting process (vacuum pressure, flow rate, achieved clamping force, etc.).
Laser solution: Marking stationscan be integrated at various points in the process chain. A pulsed, scanner-guided laser beam creates a high-contrast marking on the aluminum surface. It can be read by a camera and provide processing information to robots and machines further down the process chain.
Surface processing:
Cast aluminum components have various types of contamination on their surfaces: residues from the release agent in the casting mold (oils and fluids), as well as casting powder or smoke residue. An oxide film also forms quickly on aluminum. All of this affects the assembly steps in the rear process chain, such as welding, bonding, and sealing.
Laser solution: Scanner-guided short-pulse lasers specifically clean the relevant seam points: Oxide and contaminants are vaporized and extracted. However, that is not all: When the correct parameters are set, the laser pulses homogenize the crystalline surface structure at a micro level in preparation for subsequent sealing – no more so-called corrosion creep, making joining easier and improving quality. To prepare the surface for bonding, the laser also creates a slight texture. This little trick increases the specific surface area and greatly improves both the so-called wetting behavior and adhesive strength.